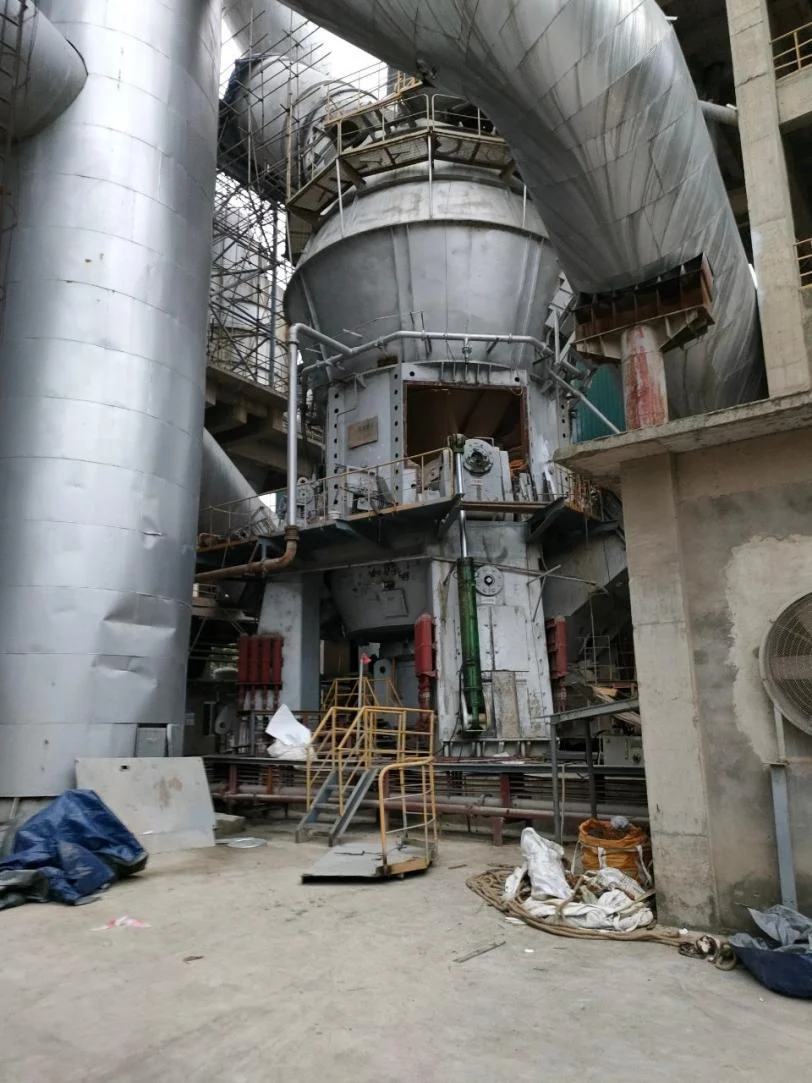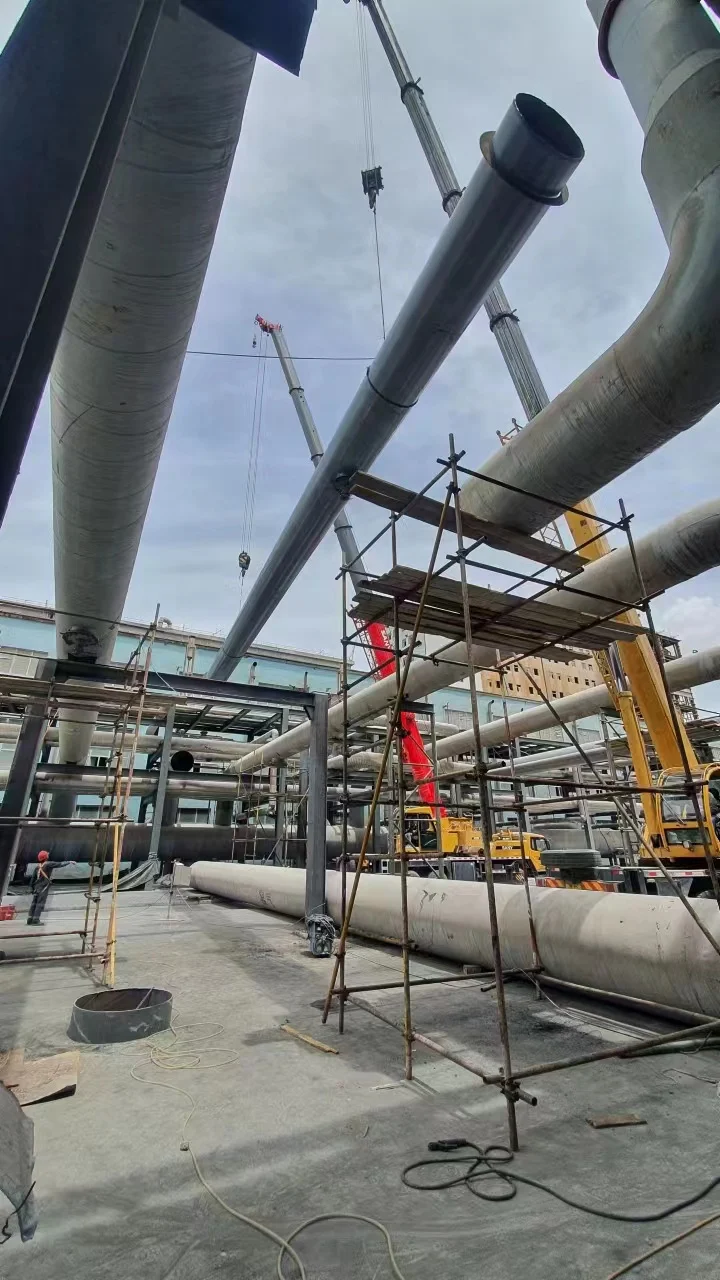
Strict restoration procedures and qualified project managers support delivery of high-quality client projects.
Business areas
Home
Product centre
Repair with new materials
Rotary-kiln inspection
Installation and maintenance
Boiler pressure piping
Machining and equipment fabrication
Contact us
Company headquartersPending confirmation
China · A16-5, Sunac Smart Valley, 555 Wenhua Avenue, Hongshan District, Wuhan, HubeiPending confirmation
Company headquartersPending confirmation
13349867738
13349867738
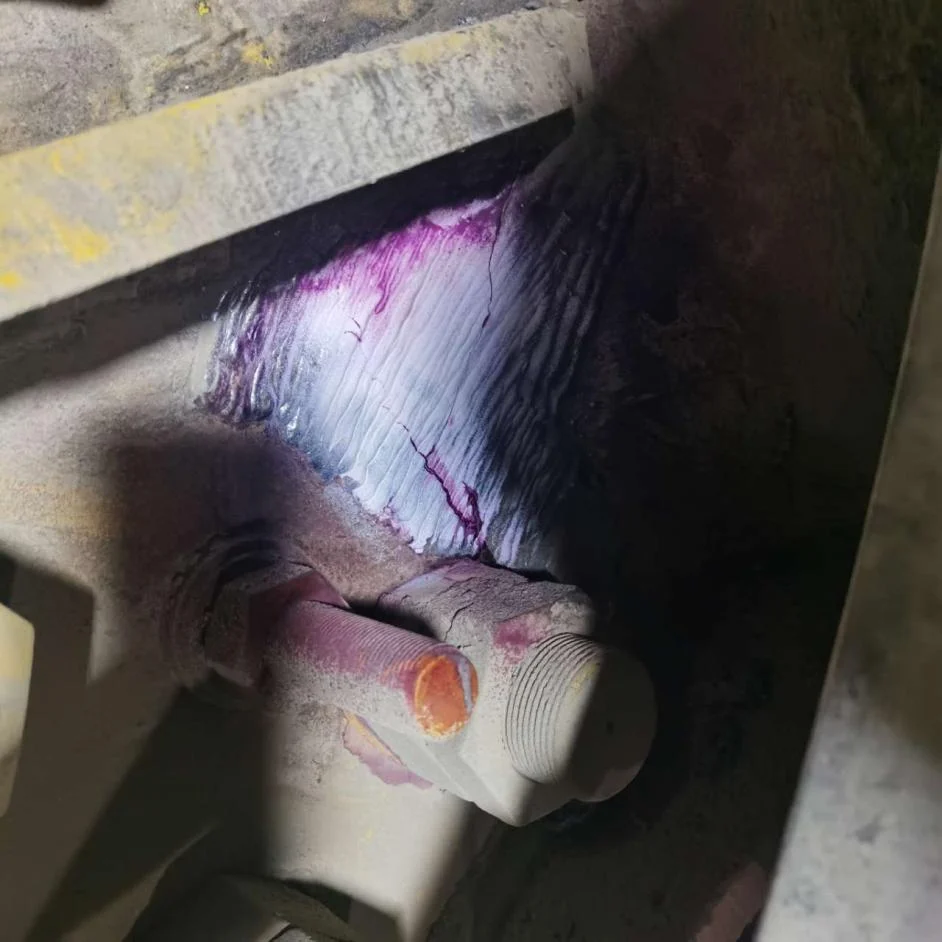
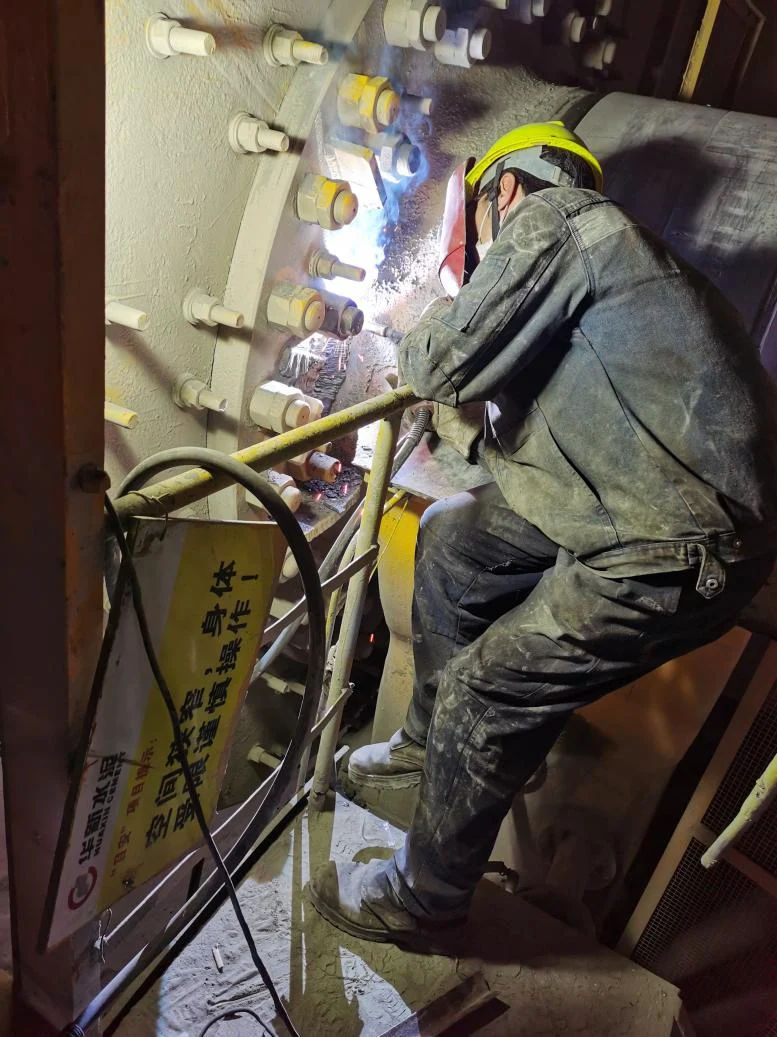
Mill end cover crack repair
Since its founding, the company has focused on technological innovation. The source describes development of FGM-KM processes and materials, frequency-modified deposition based on B.U electron-beam principles, and founder Zhang Kaiming's FGM-KM-B.U dispersion-strengthened composite functional gradient technologies, materials and processes for worn metal surface repair.
Category:
Repair with new materials
Contact telephone:
13349867738
Product enquiries
Recommended products
Detailed description
Since its founding, the company has focused on technological innovation. The source describes development of FGM-KM processes and materials, frequency-modified deposition based on B.U electron-beam principles, and founder Zhang Kaiming's FGM-KM-B.U dispersion-strengthened composite functional gradient technologies, materials and processes for worn metal surface repair.
The source lists electroplating, electroless plating, brush plating, ion bombardment, plasma spraying, spray welding, arc spraying, laser spraying, ultrasonic spray fusion, and physical and chemical vapour deposition. It claims that these methods are limited to 1-3mm coatings, with constraints in hardness, strength, toughness, thickness, mechanical, physical and chemical properties and service life.Pending confirmation
The source describes FGM-KM-B.U metal dispersion-strengthened multifunctional functional gradient material as addressing coating thickness and functional limits, depositing composite material to modify the substrate. It claims repair of fractures and damage with layers of 1-1000mm and above, improvements in toughness, hardness, strength and wear resistance, and service life increased by a factor of 1-5.Pending confirmation
(1) FGM-KM dispersion-strengthening technologyPending confirmation
The source describes FGM-KM dispersion-strengthened composite metal functional gradient materials tailored in composition and proportions to substrate and operating requirements. KM1, KM2 and KM3 alloy powders mainly contain C, Mn, Cr, W, B and Fe and are applied to gear teeth with acidic or alkaline deposition materials. Bonding, transition, working and machining layers are deposited in sequence using an immersion-fusion preparation method. It states an alloy proportion of 56.3% incorporated into substrate metal at 43.7%.Pending confirmation
(2) Specialised equipment researchPending confirmation
The source describes high-temperature laser or electron-beam deposition of FGM-KM material to form a metallurgically bonded layer for dimensional restoration and strengthening. It describes a specially modified silicon rectifier as an alternative to an expensive laser machine. The B·U deposition equipment is described as comprising a laser, power meter and guiding/focusing system that delivers high-radiance, high-brightness, directional, monochromatic energy to the workpiece. The modified rectifier is described as producing directional, bright, concentrated energy compatible with FGM-KM and the substrate, using single-pass, single-layer and multi-pass, multi-layer functional gradient deposition to build thickness.
(3) Advantages of specialised equipment research:Pending confirmation
a. The source states that laser, ultrasound and plasma methods address 1-3mm hard coatings, while the company's specialised equipment addresses multifunctional composite deposition layers of 1-1000mm and above, with property modification tailored to operating and technical requirements.Pending confirmation
b. Deposited microstructure hardness is described as 15%–50% higher than conventional quenching, with wear resistance improved 1–5 times, particularly for large, old and heavy workpieces requiring combined strengthening functions.Pending confirmation
c. Adjustments and temperature control according to material, thickness, size and shape ensure fusion between substrate and deposited zone without bursting or cracking.
d. Severely damaged, fractured, thick or extensively worn scrap workpieces can be restored efficiently on or off site with energy-saving and environmentally friendly processing.
e. Simpler equipment, operation and process steps can substantially reduce restoration cost.
Keywords: Mill end cover crack repair
Business enquiries
If you are interested in our services, complete the form below and we will contact you as soon as possible.
Submit now
Product centre
Core technology · Continuous improvement · Service projects · Progress together
Boiler pressure piping
Other equipment overhaul projects
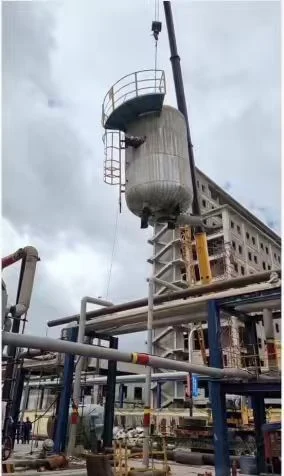
Lifting for major equipment maintenance
Pipeline replacement